

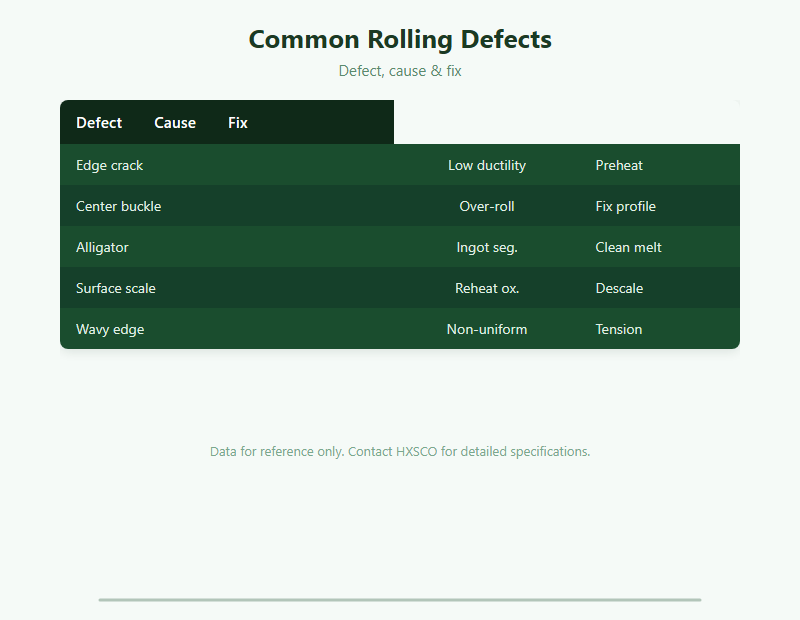
Short answer: Rolling defects — edge cracks, center buckle, alligatoring, scale and wavy edges — come from poor temperature, segregation or roll-set control. Most are avoided by clean melt practice, correct preheat and roll profiling, and caught by surface and ultrasonic inspection.
At a Glance
Where Defects Start
Hot rolling exposes Metal Inclusion Guide and Metal Dendrite Guide segregation; it follows Cold Rolling Vs Hot Rolling practice for our Steel Coil Supplier and Steel Plate Supplier.
Controlling the Mill
Preheat, descaling and roll-profile fix most issues; verify with Metal Ndt Guide and document per Mill Test Certificate Guide.
QA & Supply
Protect stock via How To Prevent Metal Rust. HXSCO supplies rolled product inspected for surface and internal soundness.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Frequently Asked Questions
A split opening at the rolling end from severe central segregation.
Low hot ductility or too-cold rolling at the edges.
More reduction at the center than the edges of the roll gap.
High-pressure descaling before and during rolling.
HXSCO supplies rolled product checked by surface and ultrasonic methods.
Source Sound-Rolled Metal from HXSCO
HXSCO supplies plate, coil and bar inspected for surface and internal soundness. Send your grade and quantity for a quote.