

Short answer: Aluminium casting defects — gas porosity, shrinkage cavities, cold shuts, oxide inclusions and misruns — trace to melt quality, pouring temperature and gating, and are fixed by drying the charge, degassing, good risering and clean pouring so the part is sound and pressure-tight.
At a Glance
Where Casting Defects Start
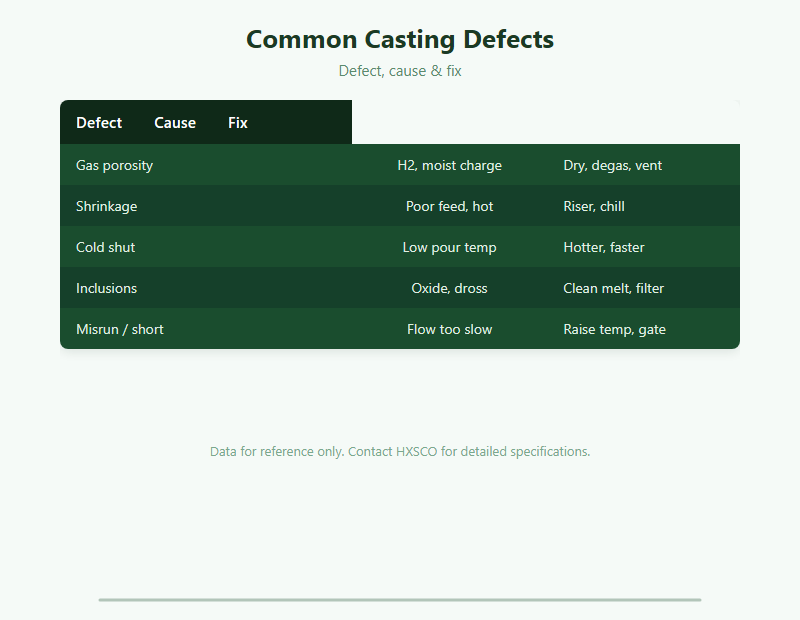
Aluminium readily absorbs hydrogen and forms oxide, so most defects begin in the melt or the pour. Porosity comes from moisture and trapped H2; shrinkage from poor feeding; cold shuts and misruns from low temperature or slow fill. The process choices are in Aluminum Die Casting Guide and Casting Supplier; the alloy basis is in Aluminum Alloy Series Guide.
Porosity, Shrinkage & Inclusions
Degas the melt, dry the charge and vent the die to kill porosity; add risers and chills to feed shrinkage; raise pour temperature and improve gating to avoid cold shuts and misruns; filter and skim to remove oxide inclusions. These controls decide whether a sand, die or Investment Casting Vs Die Casting part is sound, and pair with the density logic in Aluminum Supplier.
Inspection & Quality
X-ray and pressure-test critical castings, and inspect surfaces against the callout with Metal Ndt Guide. We supply cast stock from our Aluminum Supplier and Metal Injection Molding Guide programmes with chemistry and soundness checks and mill documentation per Mill Test Certificate Guide, packed for export.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Frequently Asked Questions
Hydrogen absorbed in the melt (from moisture or oily scrap) and poor venting; fix by drying the charge, degassing and venting the die or mould.
Two streams of metal that meet but fail to fuse because they were too cool or slow — fixed by raising pour temperature and improving gating.
Use adequate risers and chills to feed the solidifying metal, and design the part to solidify directionally toward the feed.
Oxide films and dross from a dirty melt; removed by skimming, fluxing and filtering the molten metal before pour.
HXSCO supplies aluminium castings with degassing, filtration and soundness checks (X-ray/pressure on request) and mill certificates.
Source Sound Aluminium Castings from HXSCO
HXSCO supplies aluminium castings with degassing, filtration and soundness checks on request. Send your alloy, process and quantity for a quote.