

Short answer: Creep is slow, permanent deformation of metal held under constant load at high temperature — typically above roughly 0.4 of the melting point — and it ends in stress rupture, so hot service is designed to a time-limited creep strength rather than to room-temperature yield.
At a Glance
Why Creep Happens
Below about 0.4 of a metal’s absolute melting temperature, a part loaded under its yield strength holds its shape indefinitely. Above that, atoms and dislocations gain enough thermal energy to move around obstacles, so the part slowly and permanently stretches even at a stress that would be perfectly safe cold. The room-temperature numbers from Yield Strength Vs Tensile Strength dan Tensile Test Guide therefore stop being the design limit.
Creep runs in three stages: a short primary stage where the rate falls as the metal work-hardens, a long secondary stage at a near-constant minimum rate — the number designers use — and a tertiary stage where necking and internal voids accelerate strain to rupture. Grain size matters, and coarse grains resist creep better than fine ones, the opposite of room-temperature behaviour described in Grain Structure Metals.
Designing for Hot Service
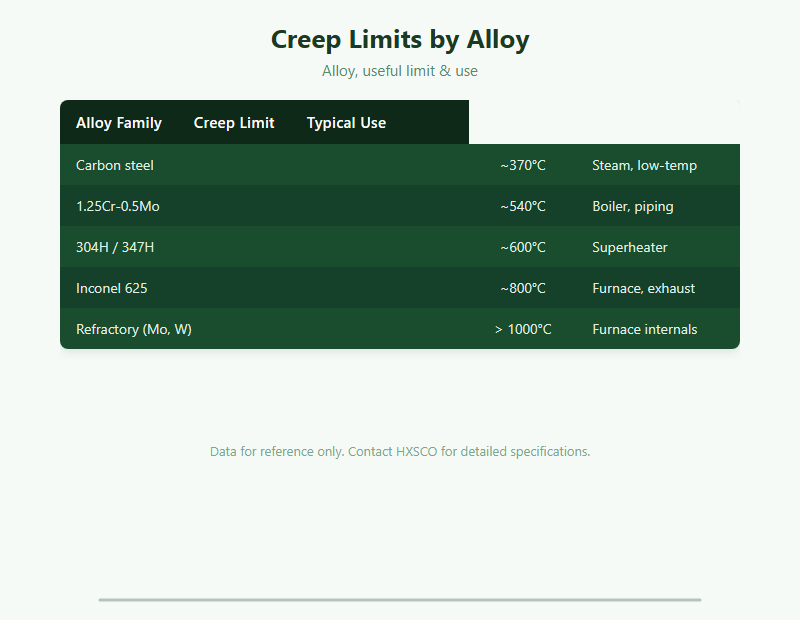
Hot design uses time-based allowables: the stress that produces 1% strain in 100,000 hours, or the stress to rupture in 100,000 hours. Carbon steel from our Carbon Steel Supplier range is limited to roughly 370 °C; chrome-moly grades in Alloy Steel Supplier extend to about 540 °C; stabilised austenitics such as 304H and 347H (see Penjelasan Nilai Baja Tahan Karat dan Stainless Steel 316 Properties) reach around 600 °C; and nickel alloys per Inconel 600 Vs 625 dan Hastelloy Guide serve to 800 °C and beyond. For furnace internals past 1000 °C the answer is our Refractory Metals Supplier range of molybdenum and tungsten.
Thermal cycling adds its own problem, because differential expansion per Thermal Expansion Of Metals loads the joint every start-up, and creep interacts with fatigue exactly as it does with corrosion in Metal Corrosion Fatigue Guide.
Testing, Inspection & Sourcing
Creep is proven by long-duration constant-load testing at temperature, reported as creep curves and Larson-Miller parameters, and extrapolated to service life. In the field, hot piping and headers are monitored for diameter growth, oxide thickness and micro-void formation using Metal Ndt Guide techniques and replica metallography. Insulated hot lines carry a second risk during shutdowns, covered in Metal Corrosion Under Insulation.
We supply creep-resisting grades in plate, pipe, bar and forgings with certified elevated-temperature data on request; forming and joining follow Forging Supplier dan Welding Consumables Guide.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Pertanyaan yang Sering Diajukan
Creep is slow, permanent deformation of a metal held under constant load at high temperature, typically above 0.4 of its absolute melting point, ending in stress rupture.
Roughly above 0.4 of the metal’s absolute melting temperature — about 370 °C for carbon steel, 540 °C for chrome-moly, 600 °C for stabilised austenitic stainless.
Primary (decreasing rate as the metal work-hardens), secondary (steady minimum rate used for design) and tertiary (accelerating strain with necking and voids, ending in rupture).
Nickel and cobalt superalloys, then stabilised austenitic stainless such as 304H and 347H, then chrome-moly steels. Refractory metals like molybdenum and tungsten serve above 1000 °C.
Yes. HXSCO supplies chrome-moly, 304H/347H, nickel alloys and refractory metals with mill certificates and elevated-temperature data on request.
Source High-Temperature Alloys from HXSCO
HXSCO supplies chrome-moly, 304H/347H, nickel and refractory alloys for creep service with certified elevated-temperature data. Send your temperature, stress and design life for a quote.