

Short answer: Stamping defects — burrs from worn tools, cracks from brittle or too-cold material, springback from elastic recovery, twist and bow from uneven stress, and surface scratches from contaminated tooling — are the main yield killers in blanking, bending and deep drawing. Most are prevented by correct tool maintenance, material temper and process design: sharpen dies, anneal before severe forming, over-bend for springback, balance the draw, and keep tooling clean, with tolerances held per ISO fits and inspected by NDT.
At a Glance
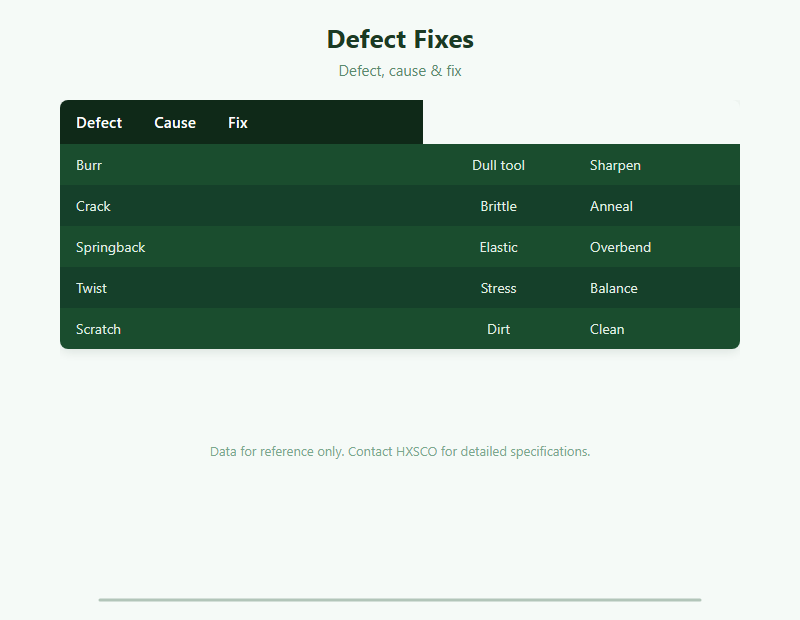
Defect Causes & Fixes
Relate to Metal Stamping Vs Machining y Metal Burr Deburring Guide; compare Metal Deep Drawing Guide y Metal Roll Forming Guide.
Calidad
Tolerance and surface checked per Metal Tolerances Fits Guide, certified by Mill Test Certificate Guide. Inspect by Metal Ndt Guide.
Supply & QA
Control springback via Metal Machinability Guide; protect via How To Prevent Metal Rust. HXSCO supplies stamping-grade coil and sheet.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Preguntas frecuentes
Dull or worn punches/dies; sharpen or regrind tooling.
Brittle temper or forming too cold; anneal first.
Over-bend past the target angle to absorb elastic return.
Uneven draw stress; balance the forming sequence.
HXSCO supplies draw-quality coil and sheet for stamping.
Source Stamping-Grade Metal from HXSCO
HXSCO supplies draw-quality steel, stainless and aluminium coil and sheet for clean stamping. Send your grade and temper for a quote.