

Short answer: Stamping defects — burrs from worn tools, cracks from brittle or too-cold material, springback from elastic recovery, twist and bow from uneven stress, and surface scratches from contaminated tooling — are the main yield killers in blanking, bending and deep drawing. Most are prevented by correct tool maintenance, material temper and process design: sharpen dies, anneal before severe forming, over-bend for springback, balance the draw, and keep tooling clean, with tolerances held per ISO fits and inspected by NDT.
At a Glance
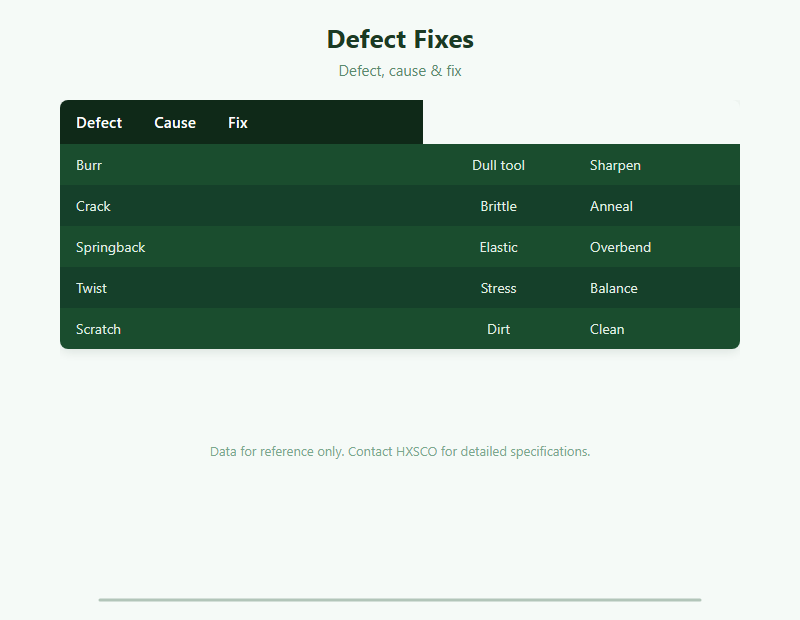
Defect Causes & Fixes
Relate to Metal Stamping Vs Machining ve Metal Burr Deburring Guide; compare Metal Deep Drawing Guide ve Metal Roll Forming Guide.
Kalite
Tolerance and surface checked per Metal Tolerances Fits Guide, certified by Mill Test Certificate Guide. Inspect by Metal Ndt Guide.
Supply & QA
Control springback via Metal Machinability Guide; protect via How To Prevent Metal Rust. HXSCO supplies stamping-grade coil and sheet.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Sıkça Sorulan Sorular
Dull or worn punches/dies; sharpen or regrind tooling.
Brittle temper or forming too cold; anneal first.
Over-bend past the target angle to absorb elastic return.
Uneven draw stress; balance the forming sequence.
HXSCO supplies draw-quality coil and sheet for stamping.
Source Stamping-Grade Metal from HXSCO
HXSCO supplies draw-quality steel, stainless and aluminium coil and sheet for clean stamping. Send your grade and temper for a quote.