

Short answer: Ultrasonic welding joins thin metal parts by pressing them between a sonotrode and anvil while 20–40 kHz vibration locally plasticises and forges the interface in under a second — no filler, flux, fumes or heat-affected zone. It is the high-speed method for battery tabs, busbars, foil packs, wire splices and electronic enclosures in copper and aluminium, and for spot-joining dissimilar thin gauges where resistance or laser welding would distort or over-penetrate.
At a Glance
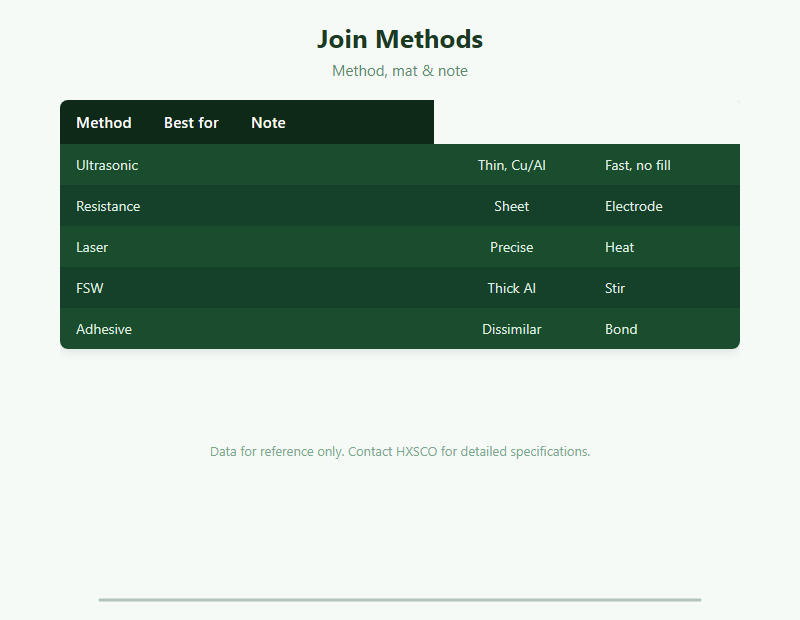
Ultrasonic vs Other
Ultrasonic joins compare with Metal Resistance Welding Guide, Metal Laser Welding Guide und Metal Friction Stir Welding Guide; relate to Metal Adhesive Bonding Guide.
Qualität
Joint and oxide checked by Metal Ndt Guide, documented per Mill Test Certificate Guide. Relate to Metal Welding Distortion Guide und Metal Heat Affected Zone Guide.
Supply & QA
Control heat via Metal Electrical Conductivity Guide; HXSCO supplies weld-ready Cu/Al strip and foil.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Häufig gestellte Fragen
Vibration forging of thin metals, no filler/heat.
Copper and aluminium foils, tabs and thin sheet.
USW is faster, cleaner, no electrode marks.
Minimal — almost no HAZ or heat distortion.
HXSCO supplies Cu/Al strip and foil for ultrasonic welding.
Source Weld-Ready Cu/Al from HXSCO
HXSCO supplies copper and aluminium strip and foil suited to ultrasonic welding. Send your alloy and gauge for a quote.