

Short answer: Carbon steel is the easiest metal to weld. MIG (ER70S-6) is fastest for sheet and production; Stick (E6010/E7018) suits field and heavy work; Flux-cored needs no gas. Match filler to grade and control heat to avoid hardness cracks.
At a Glance
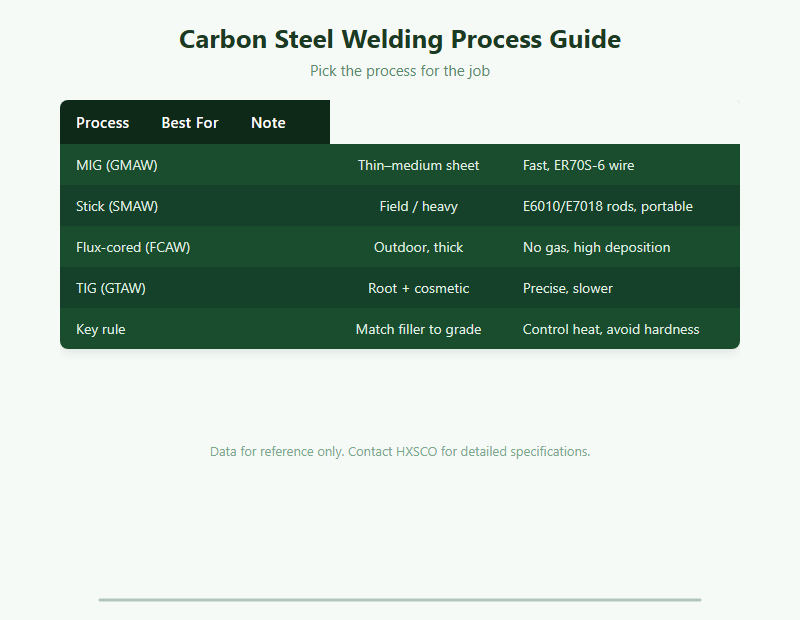
Choosing the Process
MIG is the go-to for clean shop welding of thin-to-medium carbon steel. Stick is portable for site and heavy sections. Flux-cored (FCAW) welds thick steel outdoors without shielding gas. For stainless see How To Weld Stainless Steel; for aluminum see Welding Aluminum Vs Steel.
Filler & Shielding
Use ER70S-6 MIG wire with 75/25 Ar-CO₂ or 100% CO₂, and E6010/E7018 sticks. Match filler to the base grade; for alloy steels step up to the right low-hydrogen electrode. Metal Heat Treatment Guide explains how cooling changes the weld zone.
Avoiding Common Defects
Preheat thick or high-carbon sections to avoid hard, crack-prone martensite. Keep interpass temperature controlled and use low-hydrogen consumables. Steel Pipe Fittings Flanges Guide covers joint prep for pipe.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Domande frequenti
ER70S-6 is the standard mild-steel MIG wire; pair it with 75% argon / 25% CO₂ for a stable arc and good penetration.
For thick sections or medium/high-carbon grades yes — preheat slows cooling and prevents hard, brittle, cracked weld zones.
Yes, with 309L filler for dissimilar joints, but expect different thermal expansion and corrosion behaviour at the interface.
Usually fast cooling on high-carbon steel, hydrogen from damp rods, or restraint. Preheat, use low-hydrogen consumables and control cooling.
Buy Weld-Ready Carbon Steel
HXSCO supplies A36, 1018, 1045 and A516 in plate, sheet and pipe ready for fabrication. Send your spec for a quote.