

Short answer: Welding stainless steel requires the right filler and heat control. 304 uses 308L, 316 uses 316L, 430 uses 430/309, and duplex 2205 uses 2209 filler. TIG and MIG are preferred; keep heat input low to avoid sensitization, distortion, and chromium carbide precipitation, especially with non-L grades.
At a Glance
Choosing Filler Metal
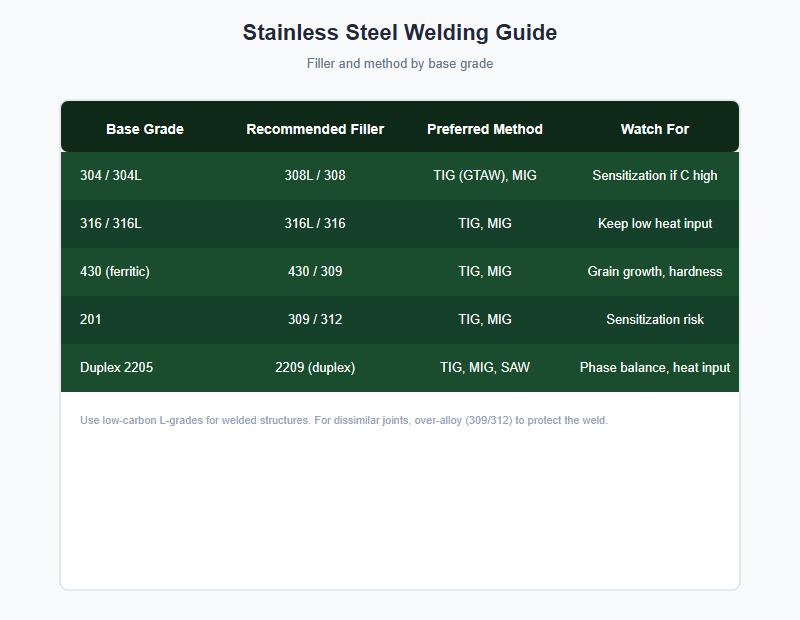
Matching or slightly over-alloying the filler prevents weak or corroded welds. The chart summarizes common pairings: 308L for 304, 316L for 316, 430/309 for ferritic 430, and 2209 duplex filler for 2205. For dissimilar joints, over-alloy with 309 or 312 to protect the weld.
Metode Pengelasan
TIG (GTAW) gives the cleanest, most controllable welds for thin sections and hygienic tube. MIG (GMAW) is faster for thicker parts and production. Stick (SMAW) is used for repair and field welds. For duplex, controlled heat input is essential to keep the phase balance.
Common Defects and How to Avoid Them
- Sensitization: Use low-carbon L-grades (304L/316L) and avoid slow cooling in the 450–850 °C range.
- Hot cracking: Keep heat input moderate and use proper filler; avoid excessive dilution.
- Distortion: Use fixtures, back-step welding, and minimal passes.
- Discoloration: Purge with argon on the back side for hygienic and high-purity welds.
Grade-Specific Tips
Ferritic 430 can grain-grow and harden; use 430 or 309 filler and avoid overheating. 201 sensitizes more easily than 304, so weld with 309/312 and control heat. Duplex 2205 needs balanced ferrite/austenite, so follow the filler and interpass-temperature limits strictly.
HXSCO supplies weld-ready 304 pipe, 316 pipe, and plate with mill certificates so your WPS matches the delivered material.
Need Material for Welding?
Tell HXSCO your grade and whether you need L-grade (welded) material, and we will supply plate, pipe, or bar with the right certificates. Request a welding-material quote.
Pertanyaan yang Sering Diajukan
Use 308L (or 308) filler for 304 base metal. Choose 308L for welded structures to reduce sensitization risk.
Use 316L (or 316) filler. For dissimilar joints to carbon steel, use 309 or 312 over-alloy filler.
Yes, but 430 is ferritic and can harden. Use 430 or 309 filler, control heat input, and avoid overheating to limit grain growth.
The low carbon reduces chromium carbide precipitation in the heat-affected zone, lowering the risk of intergranular corrosion after welding.
TIG (GTAW) gives the best control and cleanest bead on thin stainless and hygienic tubing; MIG is faster for thicker production work.
Ready to source stainless steel?
Tell us the grade, size, quantity, and destination. HXSCO will reply with a competitive quote, lead time, and mill-test options.
Request a QuoteWhy Buyers Trust HXSCO for Stainless Steel
HXSCO is a stainless steel supplier serving manufacturers, fabricators, and trading companies worldwide. We stock 304, 304L, 316, 316L, 430, 201, and duplex grades in plate, sheet, coil, pipe, tube, bar, wire, and rod forms. Every order can be supplied with mill-test certificates, third-party inspection, and custom cutting/shearing to your drawing. Contact HXSCO for a project-specific quote or material recommendation.