

Short answer: Submerged-arc welding pairs a bare wire such as EL12 or EM12K with a granular flux to make clean, deep seams at very high speed, ideal for plate and longitudinal pipe; supply in our Welding Wire Supplier and the process view in our Metal Welding Guide.
At a Glance
What SAW Does Best
SAW buries the arc under flux for no spatter, low fume and deep penetration on long seams, with the joint context in our Dissimilar Metal Welding Guide and base plate in our Carbon Steel Supplier.
Wire and Flux Pairing
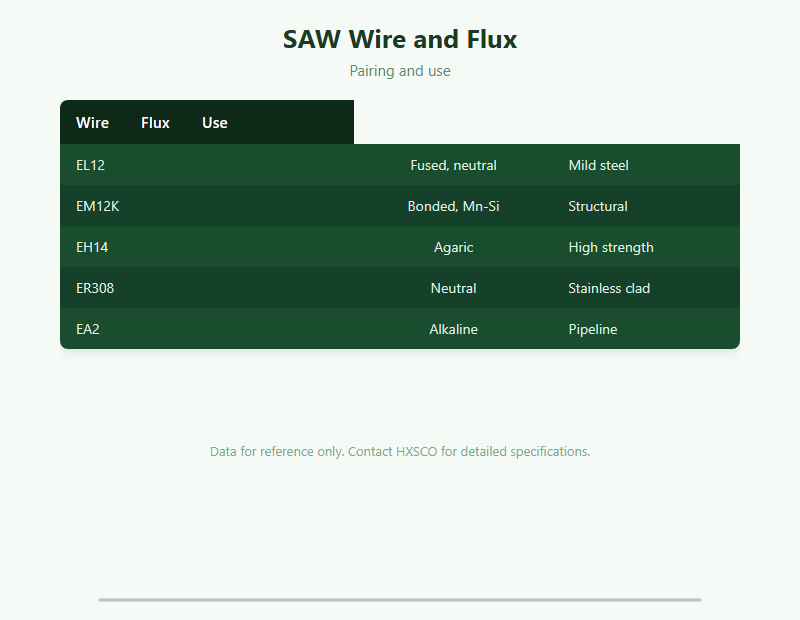
Neutral fused flux with EL12 for mild steel, and Mn-Si bonded flux with EM12K for stronger structural welds, matched to the grade.
Productivity and Quality
Single-pass deposition beats MIG several times over; verify welds with our Quality Inspection Guide and documents via our Mill Test Certificate Guide.
Tipik Uygulamalar
Pressure vessels, ship panel lines, heavy plate and longitudinal pipe, with related base forms in our Steel Pipe Supplier page.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Sıkça Sorulan Sorular
Bare wires like EL12 and EM12K.
It shields the arc and shapes the weld.
Yes – very high deposition per pass.
Stainless wire with neutral flux for cladding.
Plate, vessels, ships, pipe seams.
Get SAW Wire and Flux Quote
HXSCO supplies submerged-arc wire EL12, EM12K and matched flux with MTC. Send grade, diameter and quantity for a quote.