

Short answer: Weld thin sheet with tightly controlled heat: pulse TIG or laser for stainless and aluminium, short-arc MIG or resistance spot for steel, with good fixturing, back-purge on stainless, and clamping or skip welding to limit distortion. Match the process to thickness and alloy to avoid burn-through.
At a Glance
Heat Is the Enemy
Thin sheet has almost no thermal mass, so excess heat burns through and warps the part. Process choice follows our TIG vs MIG Guide и Laser Welding Guide; distortion is managed per our Welding Distortion Guide.
Stainless and Aluminium
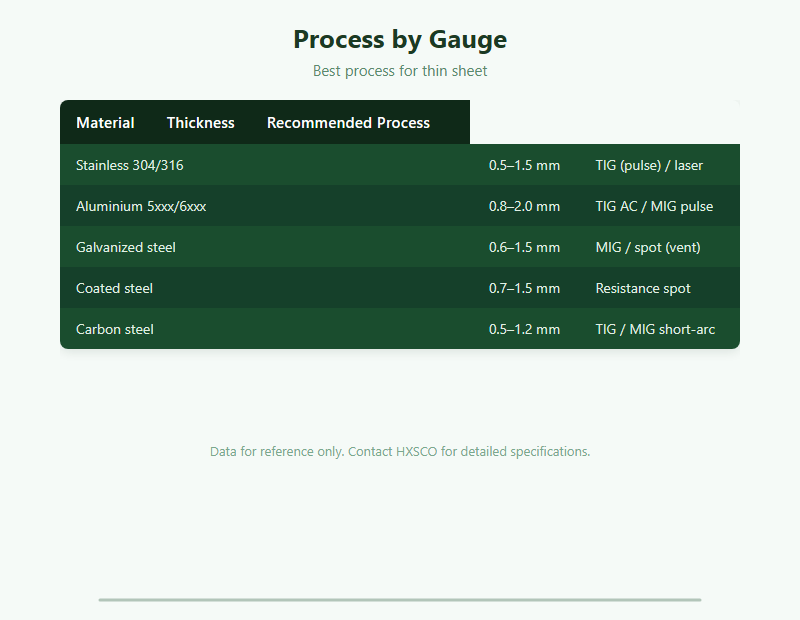
For stainless 0.5–1.5 mm use pulse TIG with argon back-purge to keep the root clean (see our Weld Stainless Guide). Aluminium needs AC TIG or pulse MIG and care with oxide; our Weld Aluminium Guide covers setup. Filler choice matters for both.
Coated and Galvanized Steel
Galvanized and coated sheet release fumes when welded, so ventilate and prefer resistance spot or short-arc MIG. Coating behaviour is in our Galvanized Supplier и Galvanizing Defects Guide; joint prep follows our Weld Edge Prep Guide.
Fixturing, Distortion and Inspection
Clamp to a heat sink, weld in short segments or skip-weld, and use copper backing where possible. Verify with the NDT methods in our NDT Guide и Weld Defects Guide. Our Stainless Sheet Supplier и Aluminium Sheet Supplier stock the thin gauges these jobs need.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Часто задаваемые вопросы
Pulse TIG with argon back-purge, or laser welding.
Lower heat input, pulse, clamp to a heat sink, weld short.
Yes — ventilate and prefer spot or short-arc MIG.
Clamp, skip-weld, sequence, and use copper backing.
By NDT: dye penetrant, UT or radiography as needed.
Get Thin-Sheet Metal from HXSCO
HXSCO stocks thin-gauge stainless, aluminium and coated sheet ready for clean welding. Send your alloy, gauge and quantity for a quote.