

Short answer: Stress relief heating at 550 to 650 C for steel removes residual stress from welding, machining and casting to prevent warping and cracking, arranged via our Heat Treatment Supplier page and paired with annealing in our Annealing Guide.
At a Glance
Why Stress Relieve
Residual stress from welding or cutting can warp or crack parts later; low-temperature heating relaxes it, with the welding context in our Metal Welding Guide and base metal in our Carbon Steel Supplier.
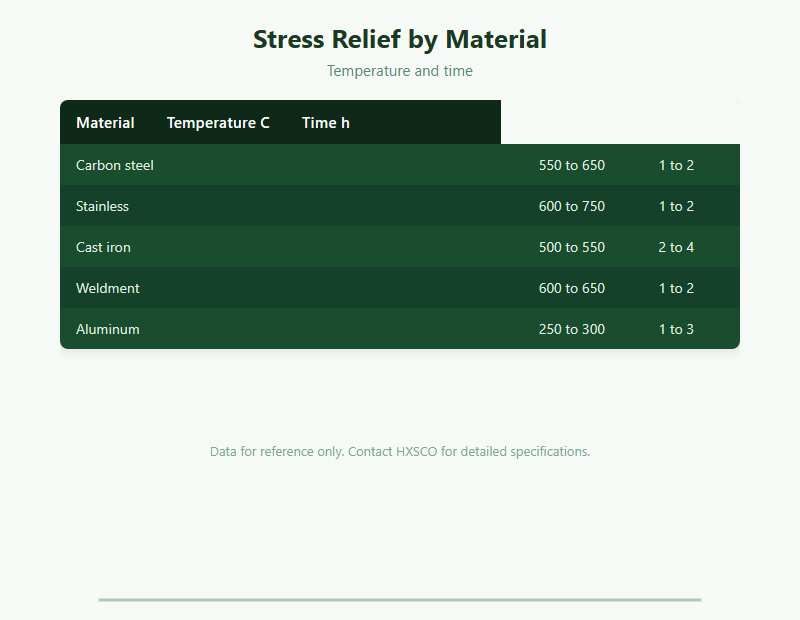
Temperature and Time by Material
Carbon steel takes 550 to 650 C, stainless 600 to 750 C and cast iron needs longer soaks, with the property basis in our Hardness and Tensile Guide.
Quality and Certification
Cycle records confirm the soak; verify with our Quality Inspection Guide and documents per our Mill Test Certificate Guide.
Get a Quote
Tell HXSCO your requirements and we will respond with a competitive quote and lead time.
Часто задаваемые вопросы
550 to 650 C.
Yes – to stop cracking.
1 to 4 hours by material.
Little – it is low temperature.
Yes – temperature record.
Get a Stress Relief Quote
HXSCO arranges stress relief for welds, castings and machined parts with cycle records. Send material and size for a quote.